16.11.2026 by Viktor Siebert
Okuma MIV04A-1-B5: Axis vibration without an alarm – practical example
The axis moves and the motor vibrates, yet the CNC displays no alarm. This symptom deserves attention. An absent alarm does not automatically mean that the drive is operating correctly. Using the Okuma MIV04A-1-B5, reference 1006-2314, as an example, we explain how intermittent vibration can be investigated systematically.
Practical example: The following sequence is an illustrative diagnostic scenario based on known MIV-series fault patterns. It is neither a customer testimonial nor a repair report for the individual unit shown.
The symptom: vibration during movement
In this example, the operator reports rough running on one axis. An initial short inspection does not reproduce the behaviour. The operator initially decides against further work. When the axis repeatedly vibrates during machine operation, the drive is sent back for a more extensive investigation.
The circumstances now matter: Does it happen at low feed rates or during acceleration? In both directions? Only after extended operation? At a particular axis position? These observations determine the next test conditions.
Why might there be no CNC alarm?
Alarm monitoring detects defined fault conditions. It does not assess every noise or irregularity in axis motion. Abnormal behaviour can therefore occur without a shutdown condition being detected. Our technical documentation records “axis/motor vibrates during movement, no CNC alarm” as a known MIV-series symptom. An internal electronics fault is documented as the cause in a different MIV model.
This makes the electronics a reasonable area to investigate. The symptom alone does not establish a defect in an MIV04A-1-B5. Mechanics, motor, cables and feedback also need consideration.
What does the MIV04A-1-B5 do?
The servo drive powers the assigned motor and operates with feedback within the axis control loop. Smooth movement requires the electrical control and mechanical system to work together. Simply establishing that the module switches on is insufficient when investigating vibration.
| Item | Details |
|---|
| Manufacturer | Okuma |
| Model | MIV04A-1-B5 |
| Reference | 1006-2314 |
| Device | Servo drive / inverter module |
| Symptom in this example | Axis or motor vibrates during movement without a CNC alarm |
A replacement enquiry requires checking the complete version and machine configuration.
How to narrow down the cause
- Make the behaviour traceable: Record direction, feed rate, position, operating time and load. A short recording from a safe distance helps relate sound to motion.
- Include mechanics and motor: Qualified personnel examine mounting, coupling, backlash, lubrication and unusual bearing noise. Replacing electronics will not correct a mechanical problem.
- Check supply, wiring and feedback: Connections, motor cable and feedback path are examined using the appropriate machine documentation. Changing parameters is not a sensible first experiment when a previously smooth system suddenly starts vibrating.
- Extend the test conditions: A suitable, safely configured test setup is used to investigate the reported movements and different operating conditions. A brief power-on check is often insufficient for an intermittent fault.
Illustrative diagnosis and repair approach
In this scenario, vibration returns only during the extended investigation. Comparative testing with a verified compatible setup narrows the cause down to the drive electronics. The affected area is repaired and the drive tested again.
The final check must revisit the conditions that previously produced the symptom. Does motion remain smooth during repeated movements? Does it remain stable after warming up? Starting without an alarm would not be sufficient evidence. Operation together with the machine must also be checked after reinstallation.
What can the operator do?
- Safely stop operation and involve maintenance if vibration is new or severe.
- Record the affected axis, direction, feed rate, operating time and whether the system is cold or warm.
- Explicitly record that there is no alarm. If a message subsequently appears, photograph the full display before resetting it.
- Note any preceding collision, maintenance, motor replacement or parameter change.
- Avoid speculative parameter adjustments and never disconnect plugs while the equipment is powered.
Prevention: notice changes early
Check accessible filters and external air passages according to the machine’s maintenance schedule. Pay attention to changes in fan and operating noise. Follow the specified lubrication and maintenance intervals for the axis mechanics, and report new chatter marks or increasingly rough movement promptly. Work inside the electrical cabinet, on the drive and on electrical connections belongs to qualified personnel.
These measures support early detection and reduce avoidable stress. They cannot guarantee prevention of an internal electronics failure.
Sources and technical basis
The specific symptom without a CNC alarm comes from industrypart’s internal technical documentation for the Okuma MIV series. It does not establish an identical defect in the unit pictured. Servo manufacturers also discuss mechanical resonance and relevant diagnostic checks; settings for other drive series must not be transferred to this unit.
Okuma on preventive filter maintenance: https://www.okuma.com/blog/tip-let-your-machine-tool-breathe
Okuma on vibration and suitable servo control: https://www.okuma.co.jp/english/solution_technology/servo-navi/. This describes newer functions and does not establish their availability on a machine with an MIV04A-1-B5.
Diagnosis and repair at industrypart
Does your Okuma axis vibrate without displaying an alarm? Send us the model designation, a nameplate photograph and an accurate description of the behaviour. These details help us prepare a suitable investigation and agree the scope of repair with you.
Video: axis vibration without a CNC alarm
The video explains the illustrative diagnostic approach, useful observations and preventive measures. The labelled original footage shows a device inspection and does not establish the repair sequence described.
Device photographs for this practical example
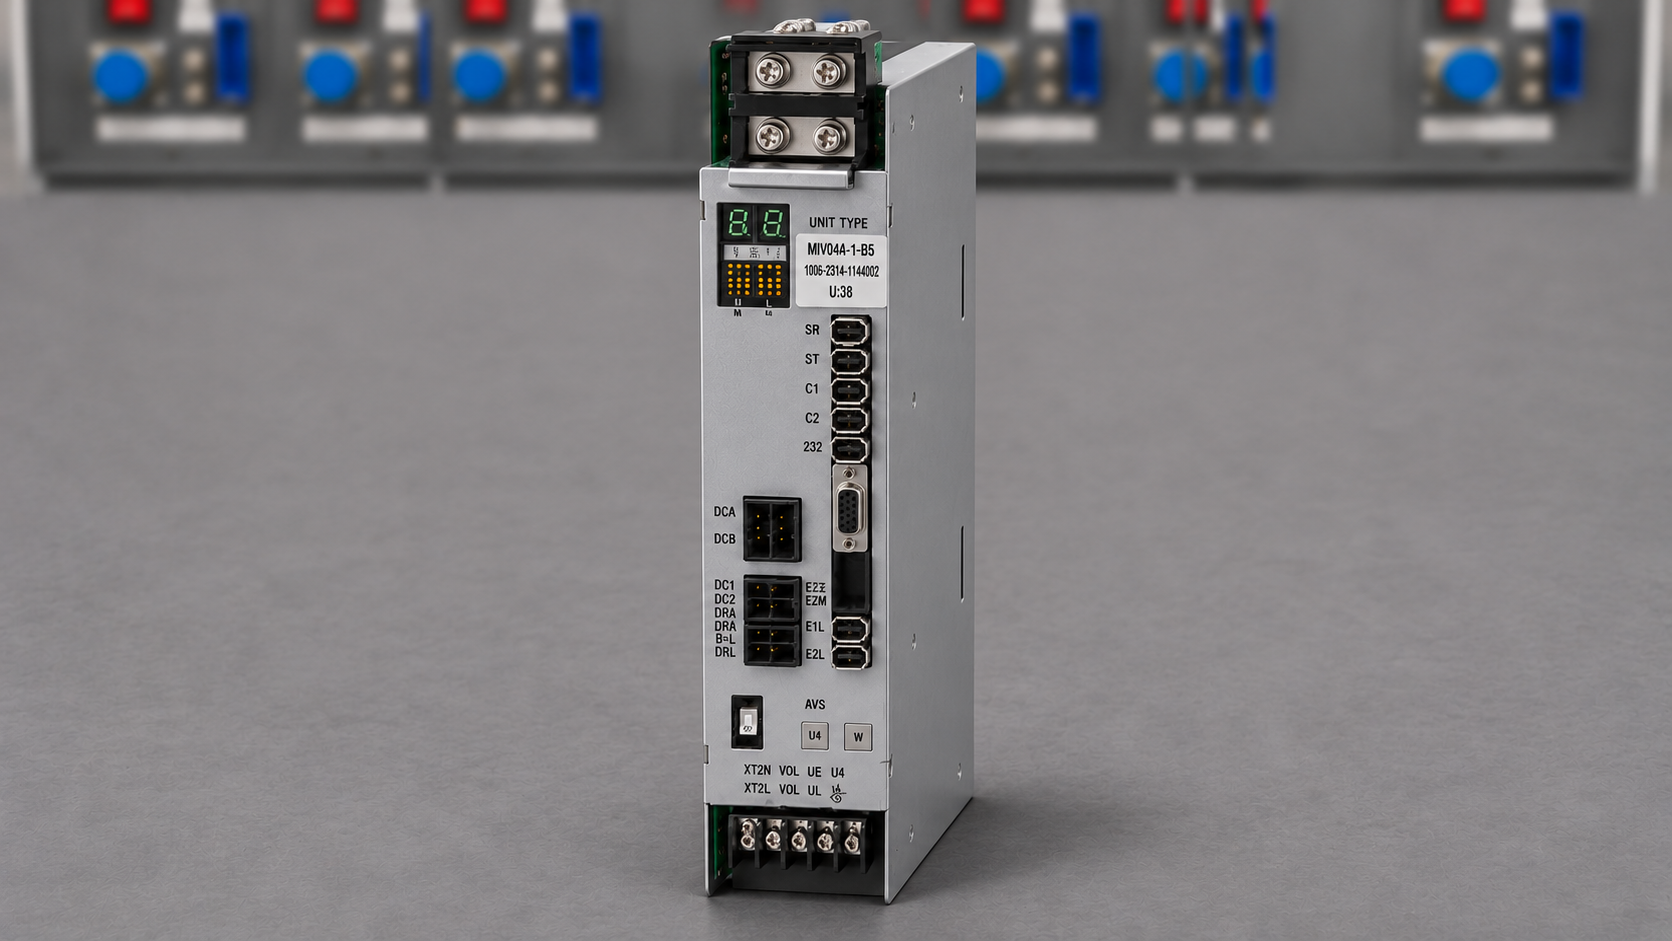 Okuma MIV04A-1-B5 shown upright at the industrypart test bench.
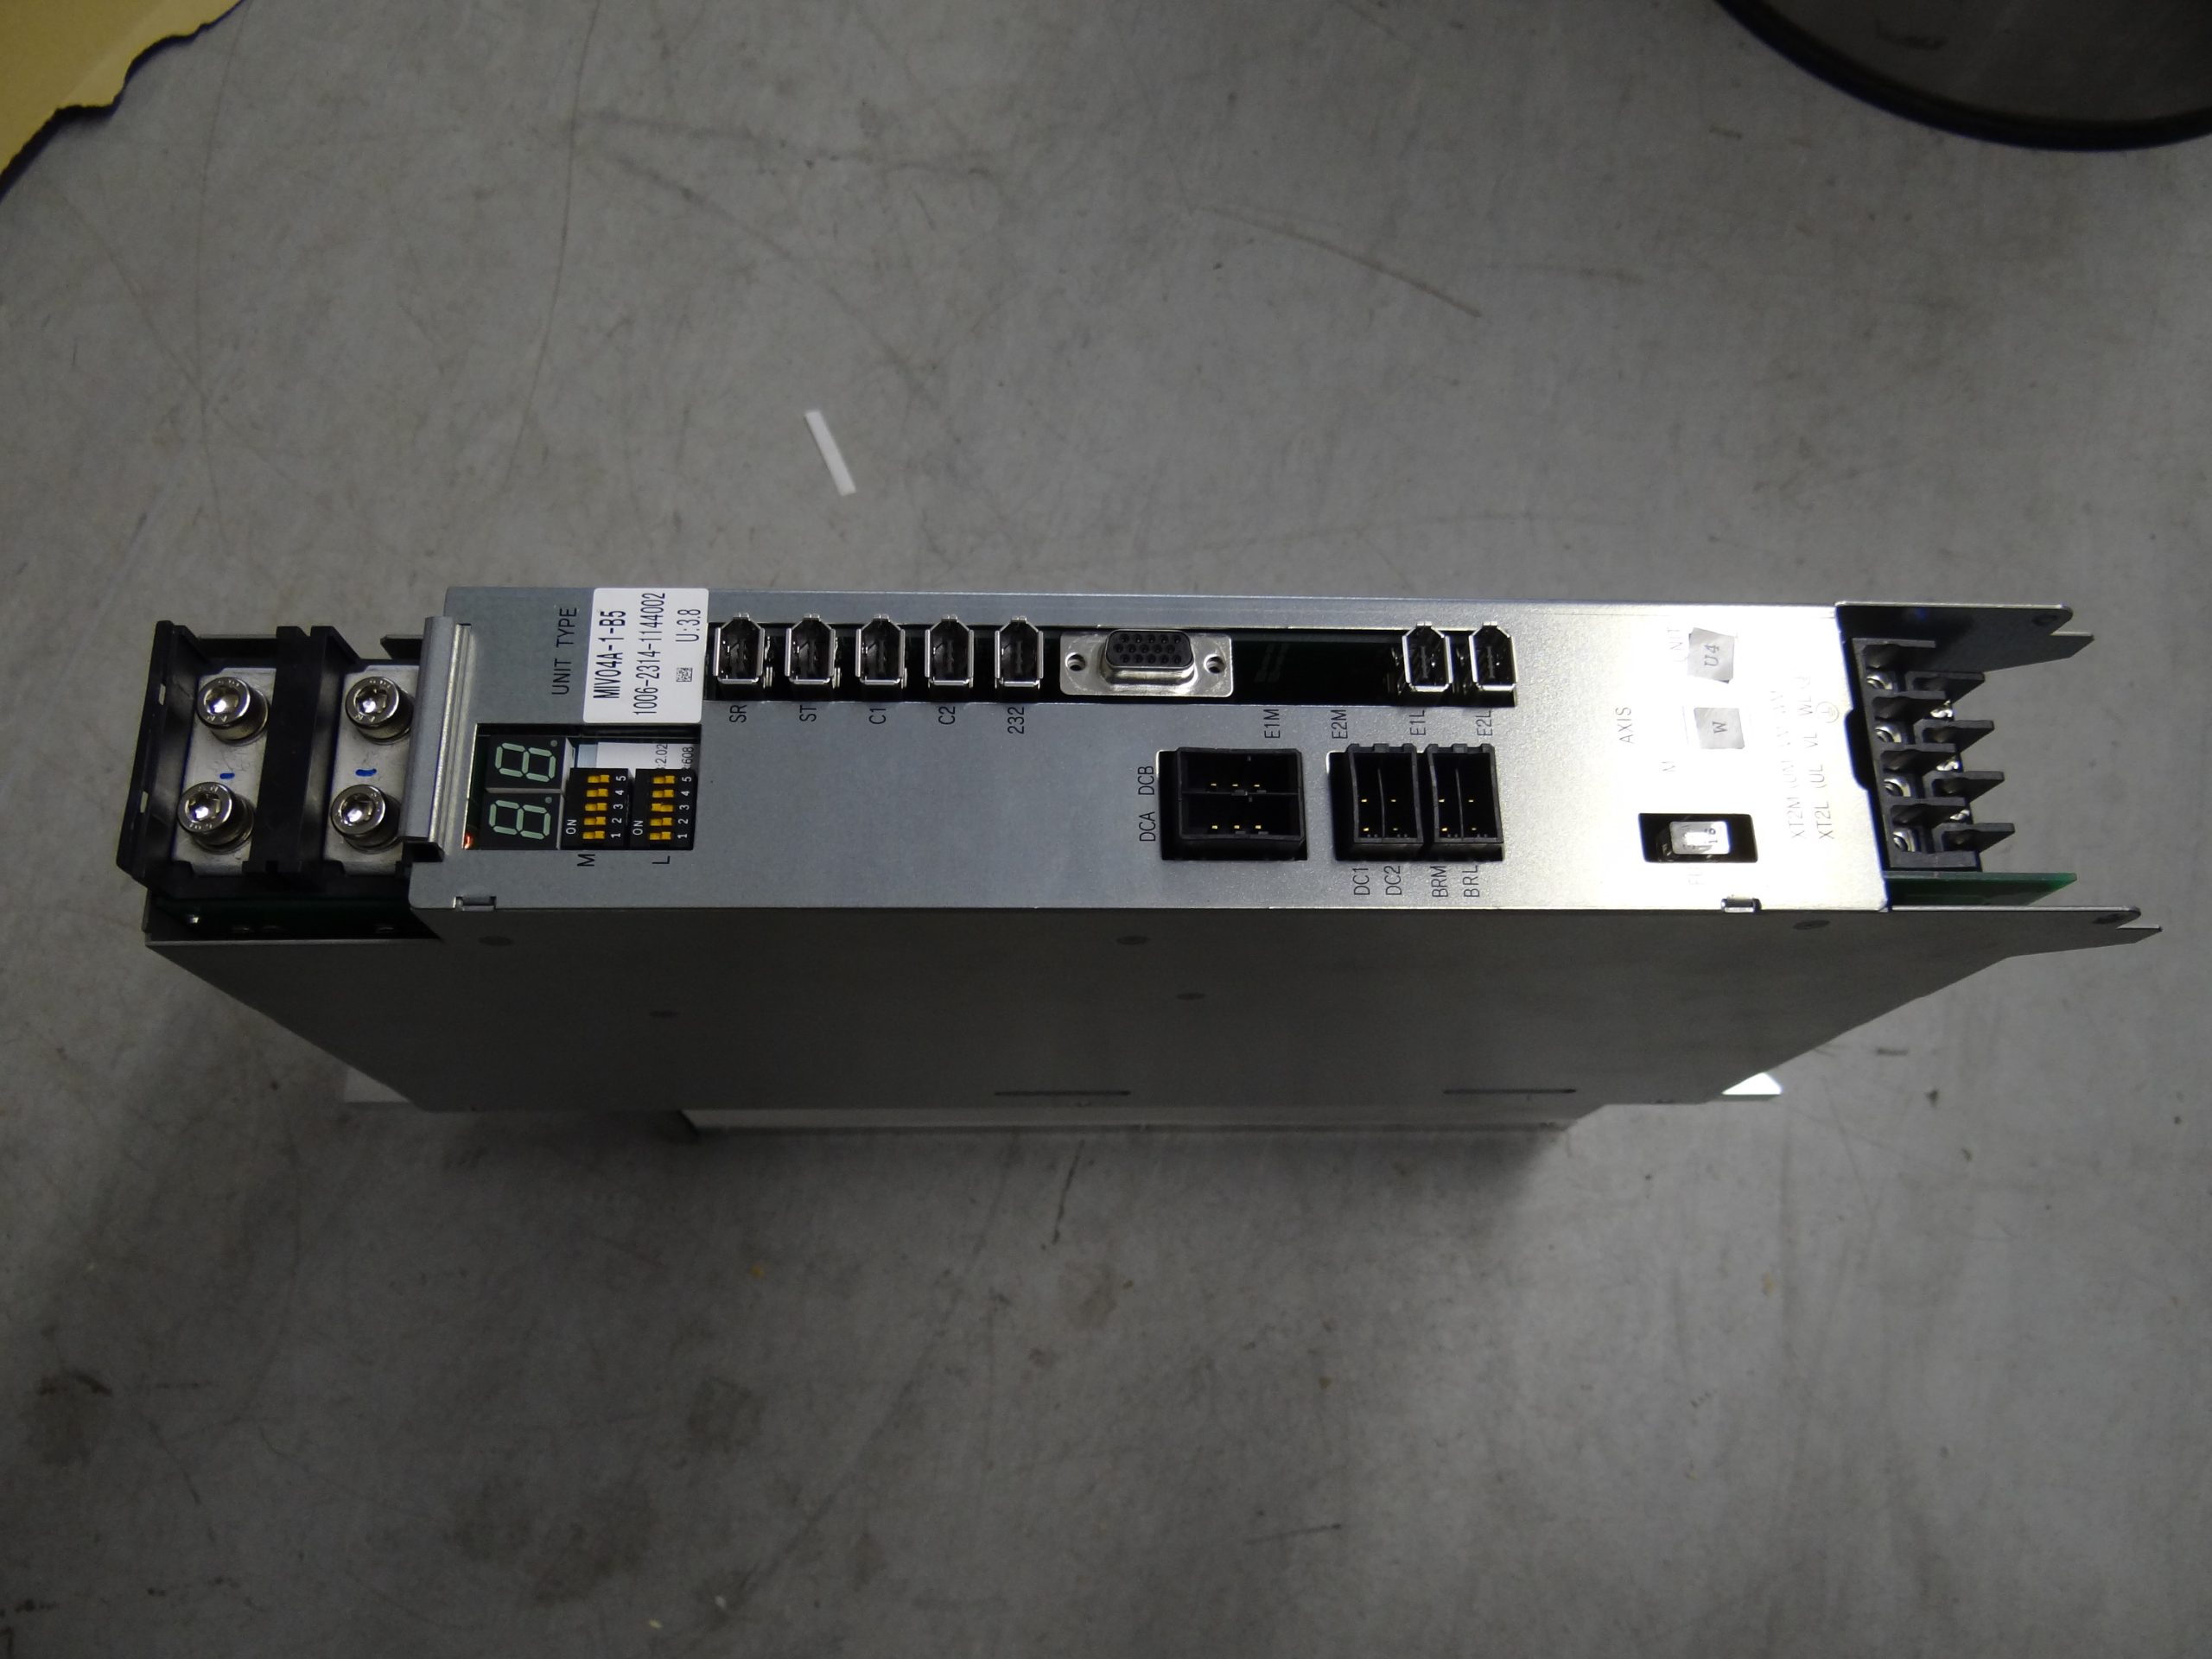 Okuma MIV04A-1-B5 on arrival, on the original surface.
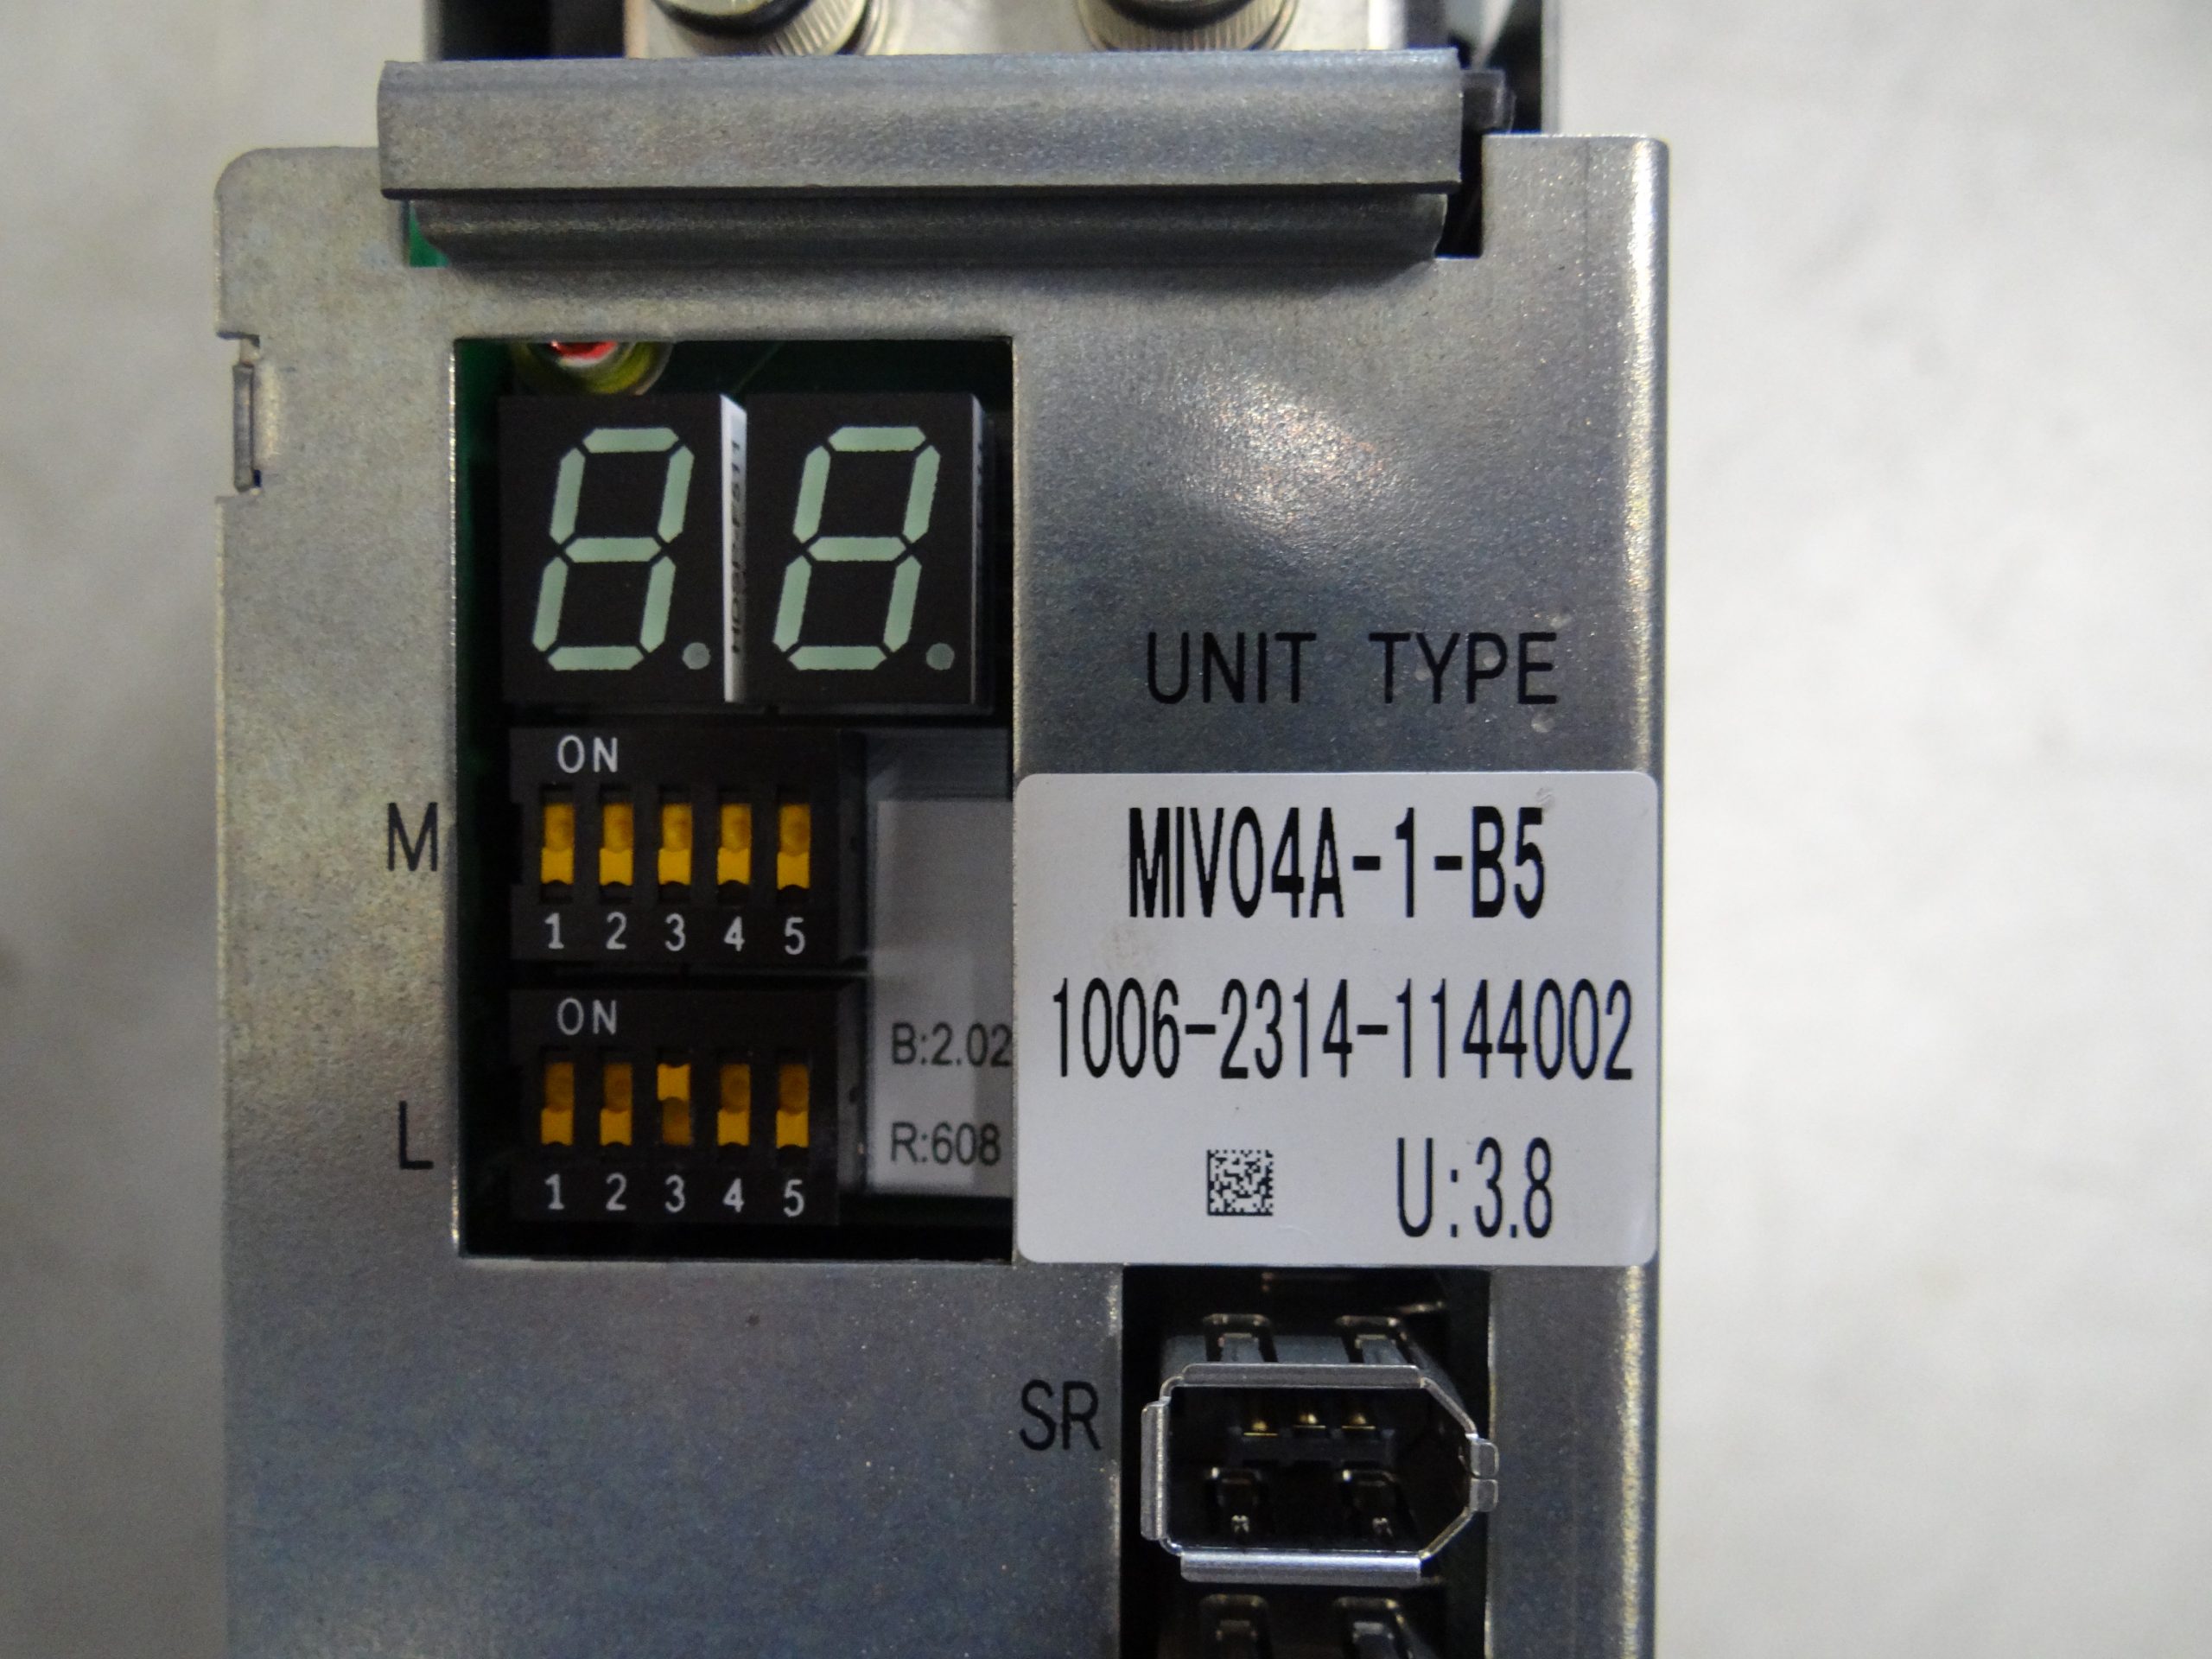 Original nameplate showing model and reference 1006-2314.
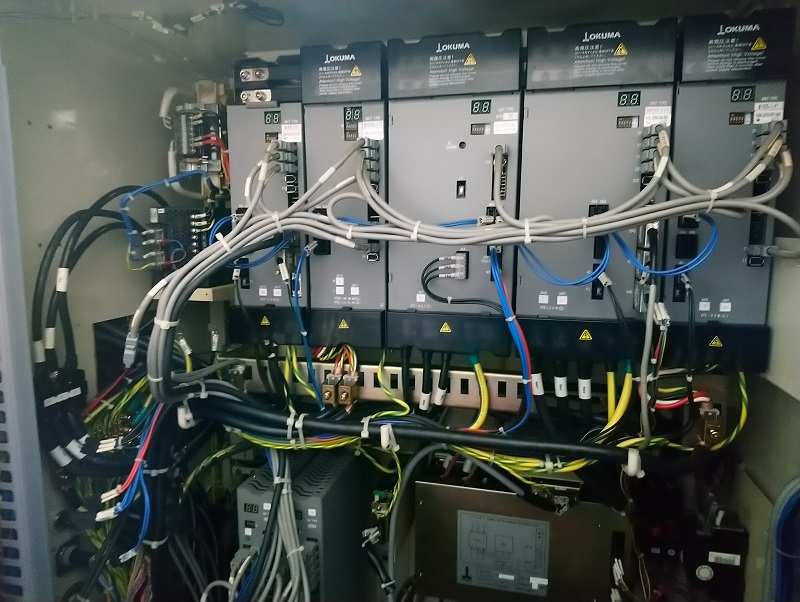 Installation photograph supplied with the customer case.
Enquire about the Okuma MIV04A-1-B5
Would you like your drive inspected or repaired? Send us a nameplate photograph and a description of the fault. You can find the corresponding product here:
https://www.industrypart.com/products/okuma-miv04a-1-b5-or-1006-2314-servo-drive-42346.html