13.11.2026 by Viktor Siebert
FANUC A06B-6055-H212: blown F7 fuse and spindle failure
A blown spindle-drive fuse can bring a CNC machine to a complete stop. Before restarting a FANUC A06B-6055-H212, establish whether the fuse has operated because of a fault in the drive or in the connected system. This documented workshop case illustrates why the power stage, control circuitry and motor should be considered together.
Customer report and symptoms
The customer reported “OT103 FUSE F7 Blew (Spindle AMP)” after another failure. This message identifies fuse F7. Record the machine message separately from the indication on the drive. An AL03 actually observed on the drive is not documented in this job.
Device, function and application
The A06B-6055-H212 is a FANUC AC Spindle Servo Unit for the spindle motor of a CNC machine tool. It converts the CNC speed command into motor power and uses the specified feedback for control and monitoring. Motor matching, spindle orientation and machine functions depend on the exact configuration and wiring.
| Item | Documented information |
|---|
| Manufacturer | FANUC |
| Device | A06B-6055-H212 |
| Type | AC Spindle Servo Unit |
| Documentation | FANUC B-53425E/09, digital type, MODEL 3 to 40 |
| Customer motor tested | FANUC A06B-0726-B402#5000 |
| Recorded test | Customer motor operation up to 6,000 rpm; satisfactory result |
The recorded test speed is not a universal rating for every drive and motor combination. Refer to the complete unit specification, motor data and machine documentation. Rated current, input voltage and output power cannot be reliably established from the available nameplate photograph.
Workshop findings and repair
Inspection found a short circuit in the power stage and damage to its associated control circuitry. Both functional groups were repaired and the channels checked successfully. Tests followed with a workshop motor and with the customer’s motor.
The final record confirms repair and successful testing with the customer’s motor. The original cause of the repeated damage could not be conclusively established. A suspected encoder fault was not confirmed as the cause.
Troubleshooting the complete system
Qualified technicians should record the exact message, the indication on the drive and the operating state: startup, acceleration, braking or operation after warming up. Supply, motor cables, connections, cooling and the actual feedback arrangement should then be checked against the relevant documentation.
A separate spindle encoder may serve the CNC while motor control uses another feedback path. A supplied encoder therefore does not automatically prove that it directly regulates the spindle drive. Confirm the wiring from the machine diagram. Open-drive work requires qualified personnel and due consideration of stored DC-link energy.
Final test and prevention
Operation with the customer’s motor up to 6,000 rpm was recorded as satisfactory. No defined endurance test or load profile is documented. Checks of the machine installation and its real operating conditions remain necessary before returning to production.
Clear cooling passages, sound connections and regular cable inspection help identify avoidable stress. Repeated fuse operation calls for systematic diagnosis before further operation.
Sources
Workshop example: repair and test documentation from 2021. General alarm references: FANUC Maintenance Manual B-53425E/09, chapter II, section 5, printed pages 98 to 99. These codes apply to the documented digital series and must be checked against the actual configuration.
https://vtda.org/docs/other/FANUC/B-53425E09_AC_Spindle_Servo_Unit_1981.pdf
Video and photographs
FANUC A06B-6055-H212: repair and testing at our workshop.Watch on YouTube: https://www.youtube.com/watch?v=9IaqqABmr-o
The media show the unit and excerpts from the original test recordings for this repair job.
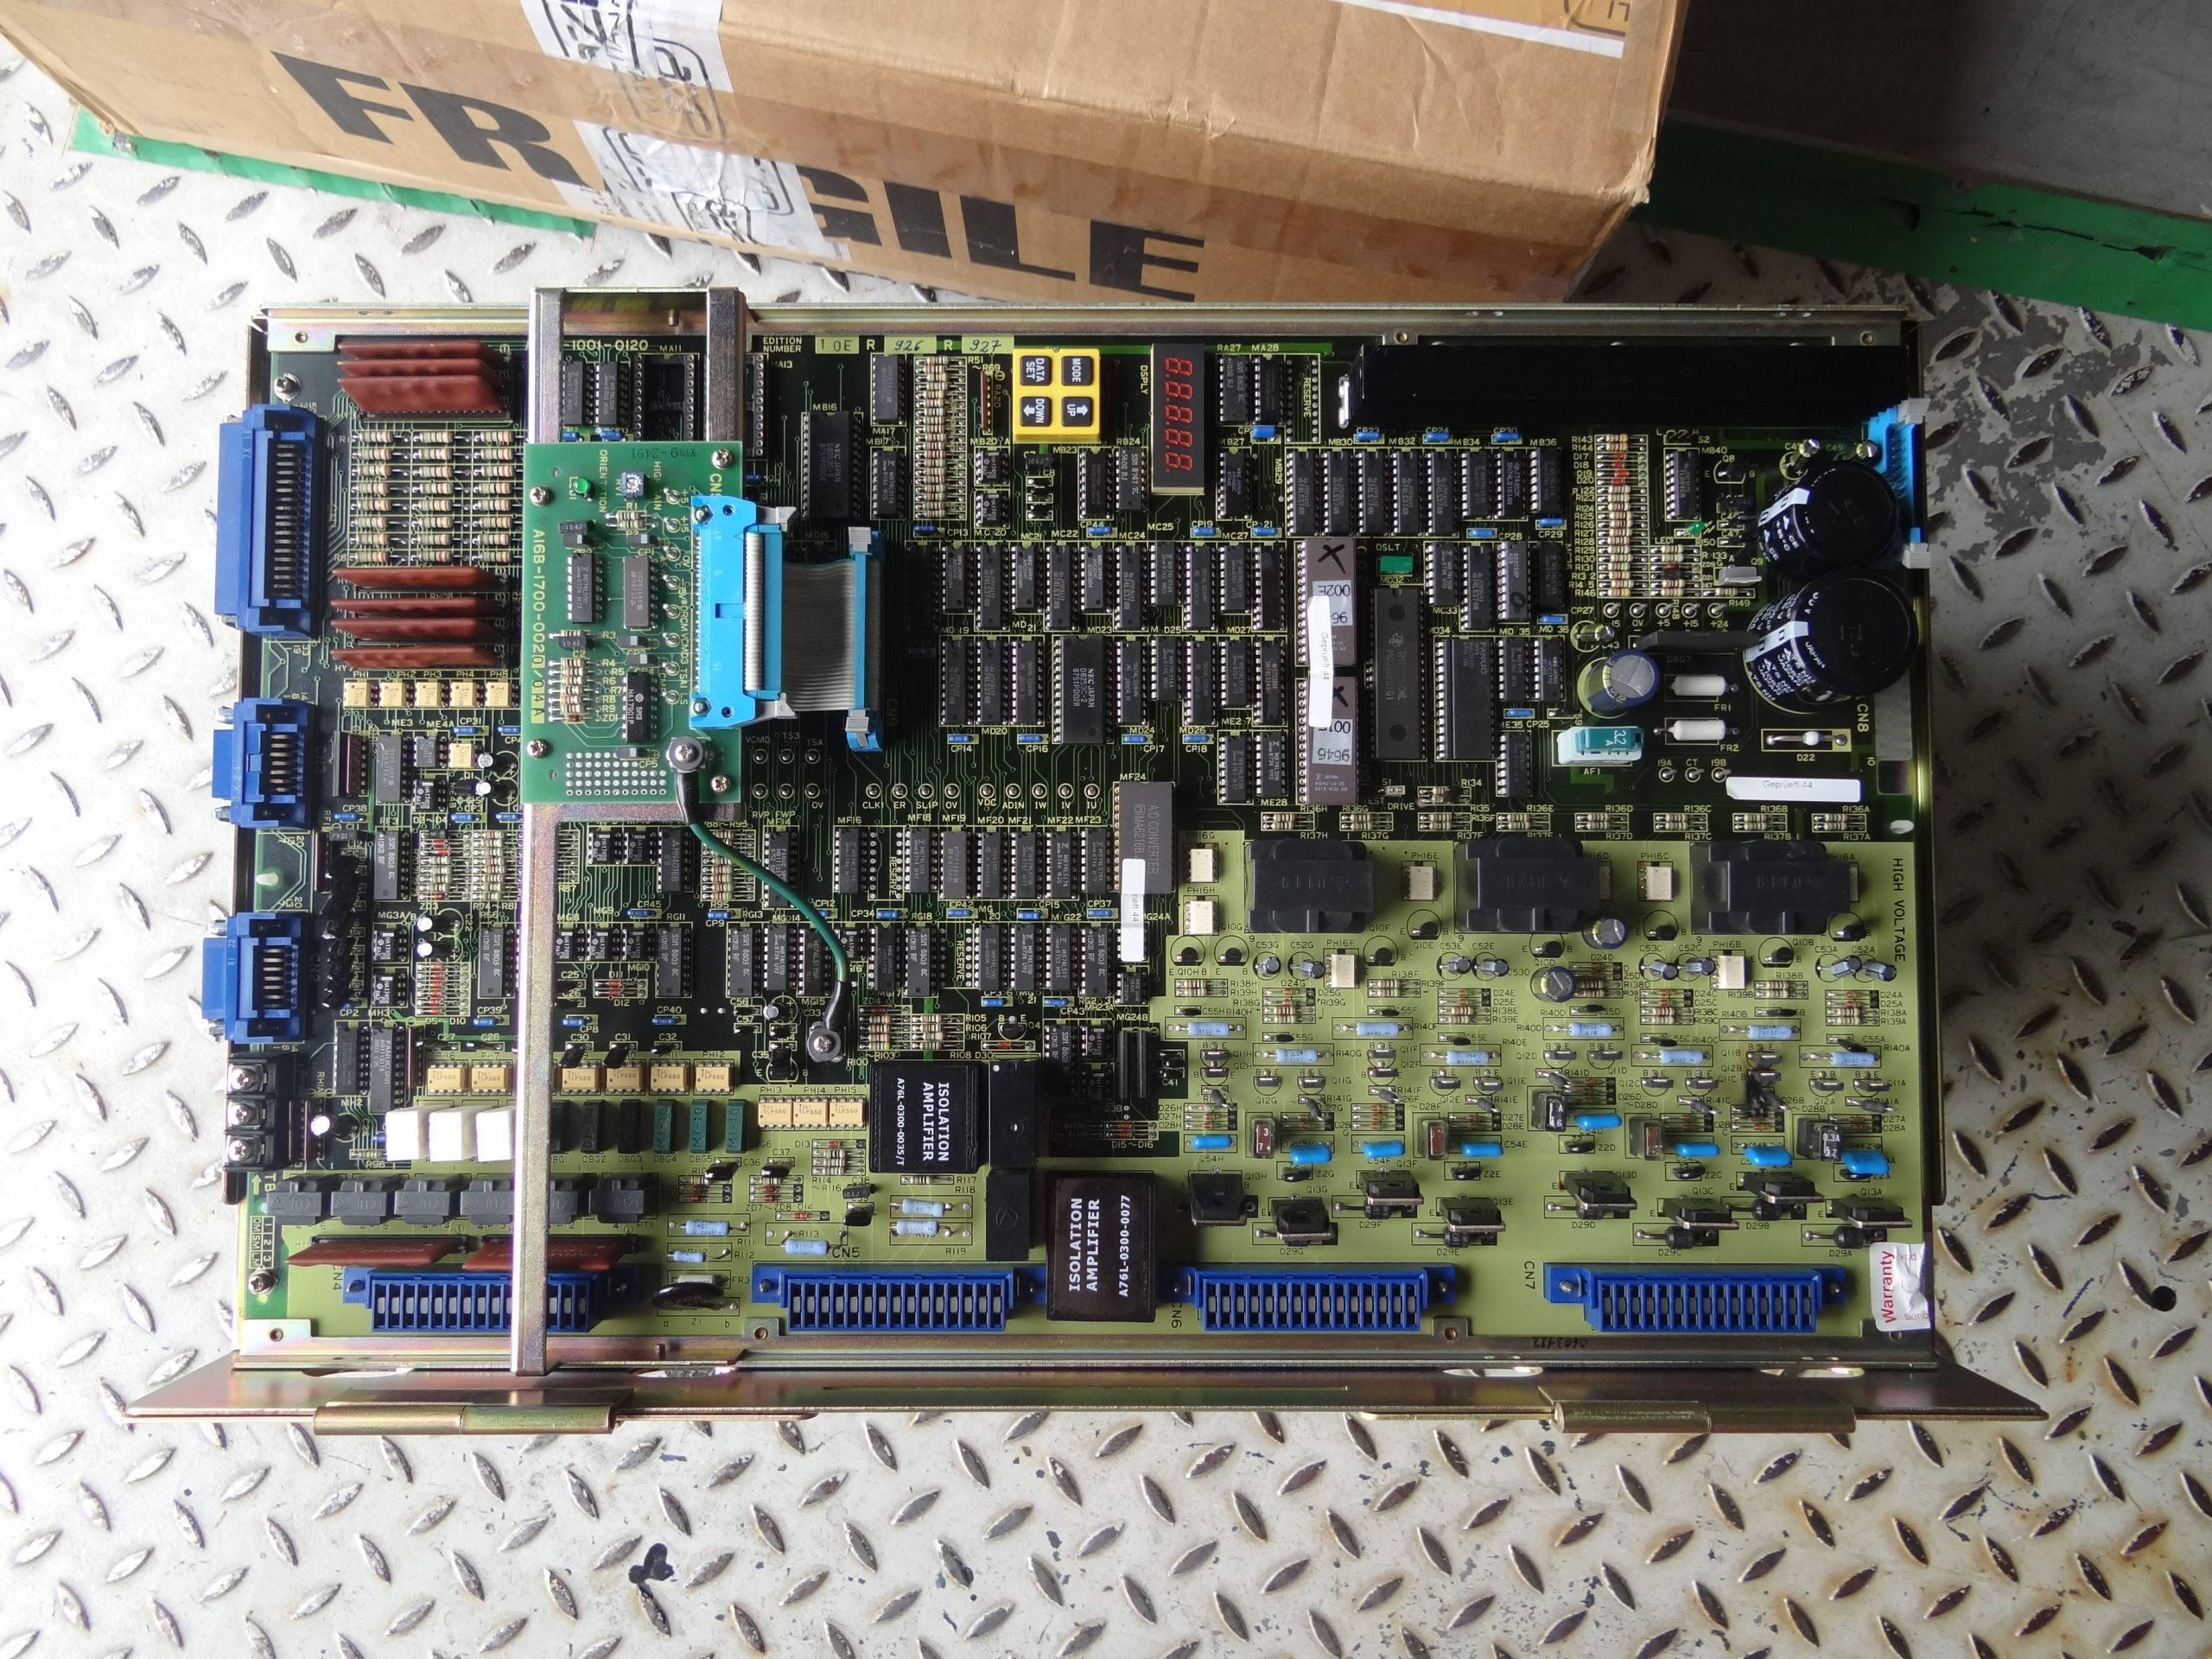 FANUC A06B-6055-H212 before repair, overall view.
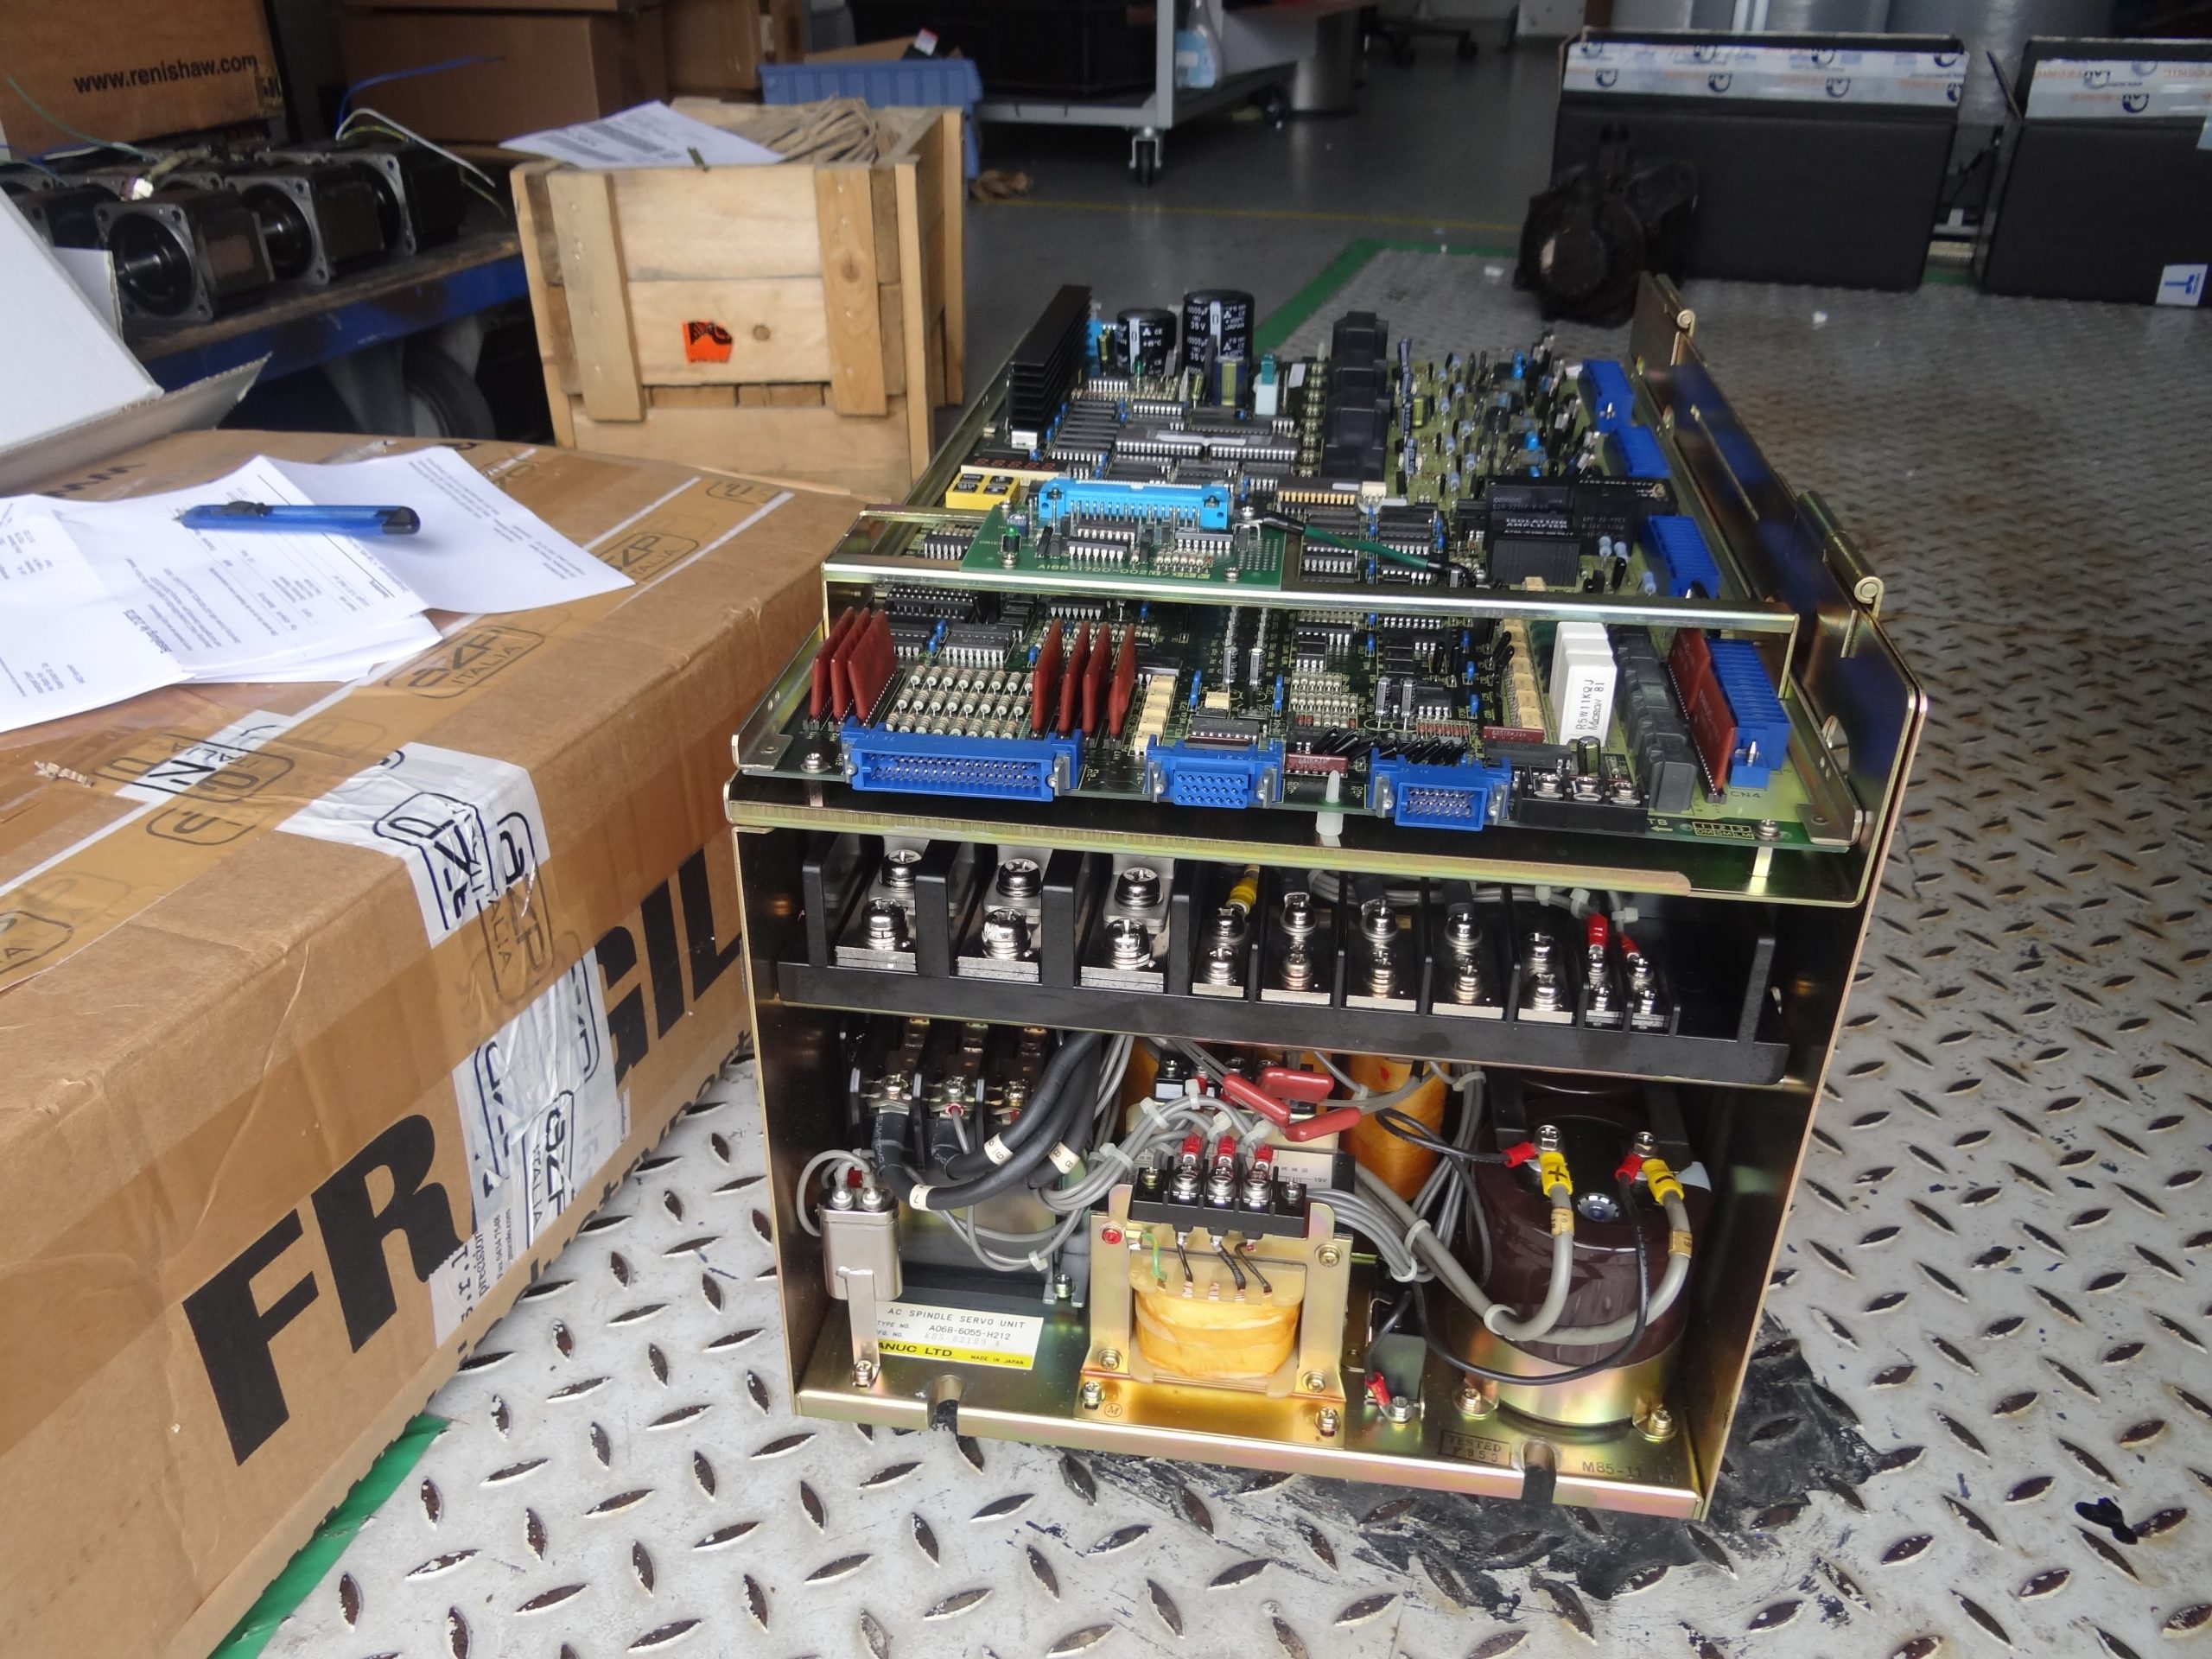 FANUC A06B-6055-H212 before repair, connection side.
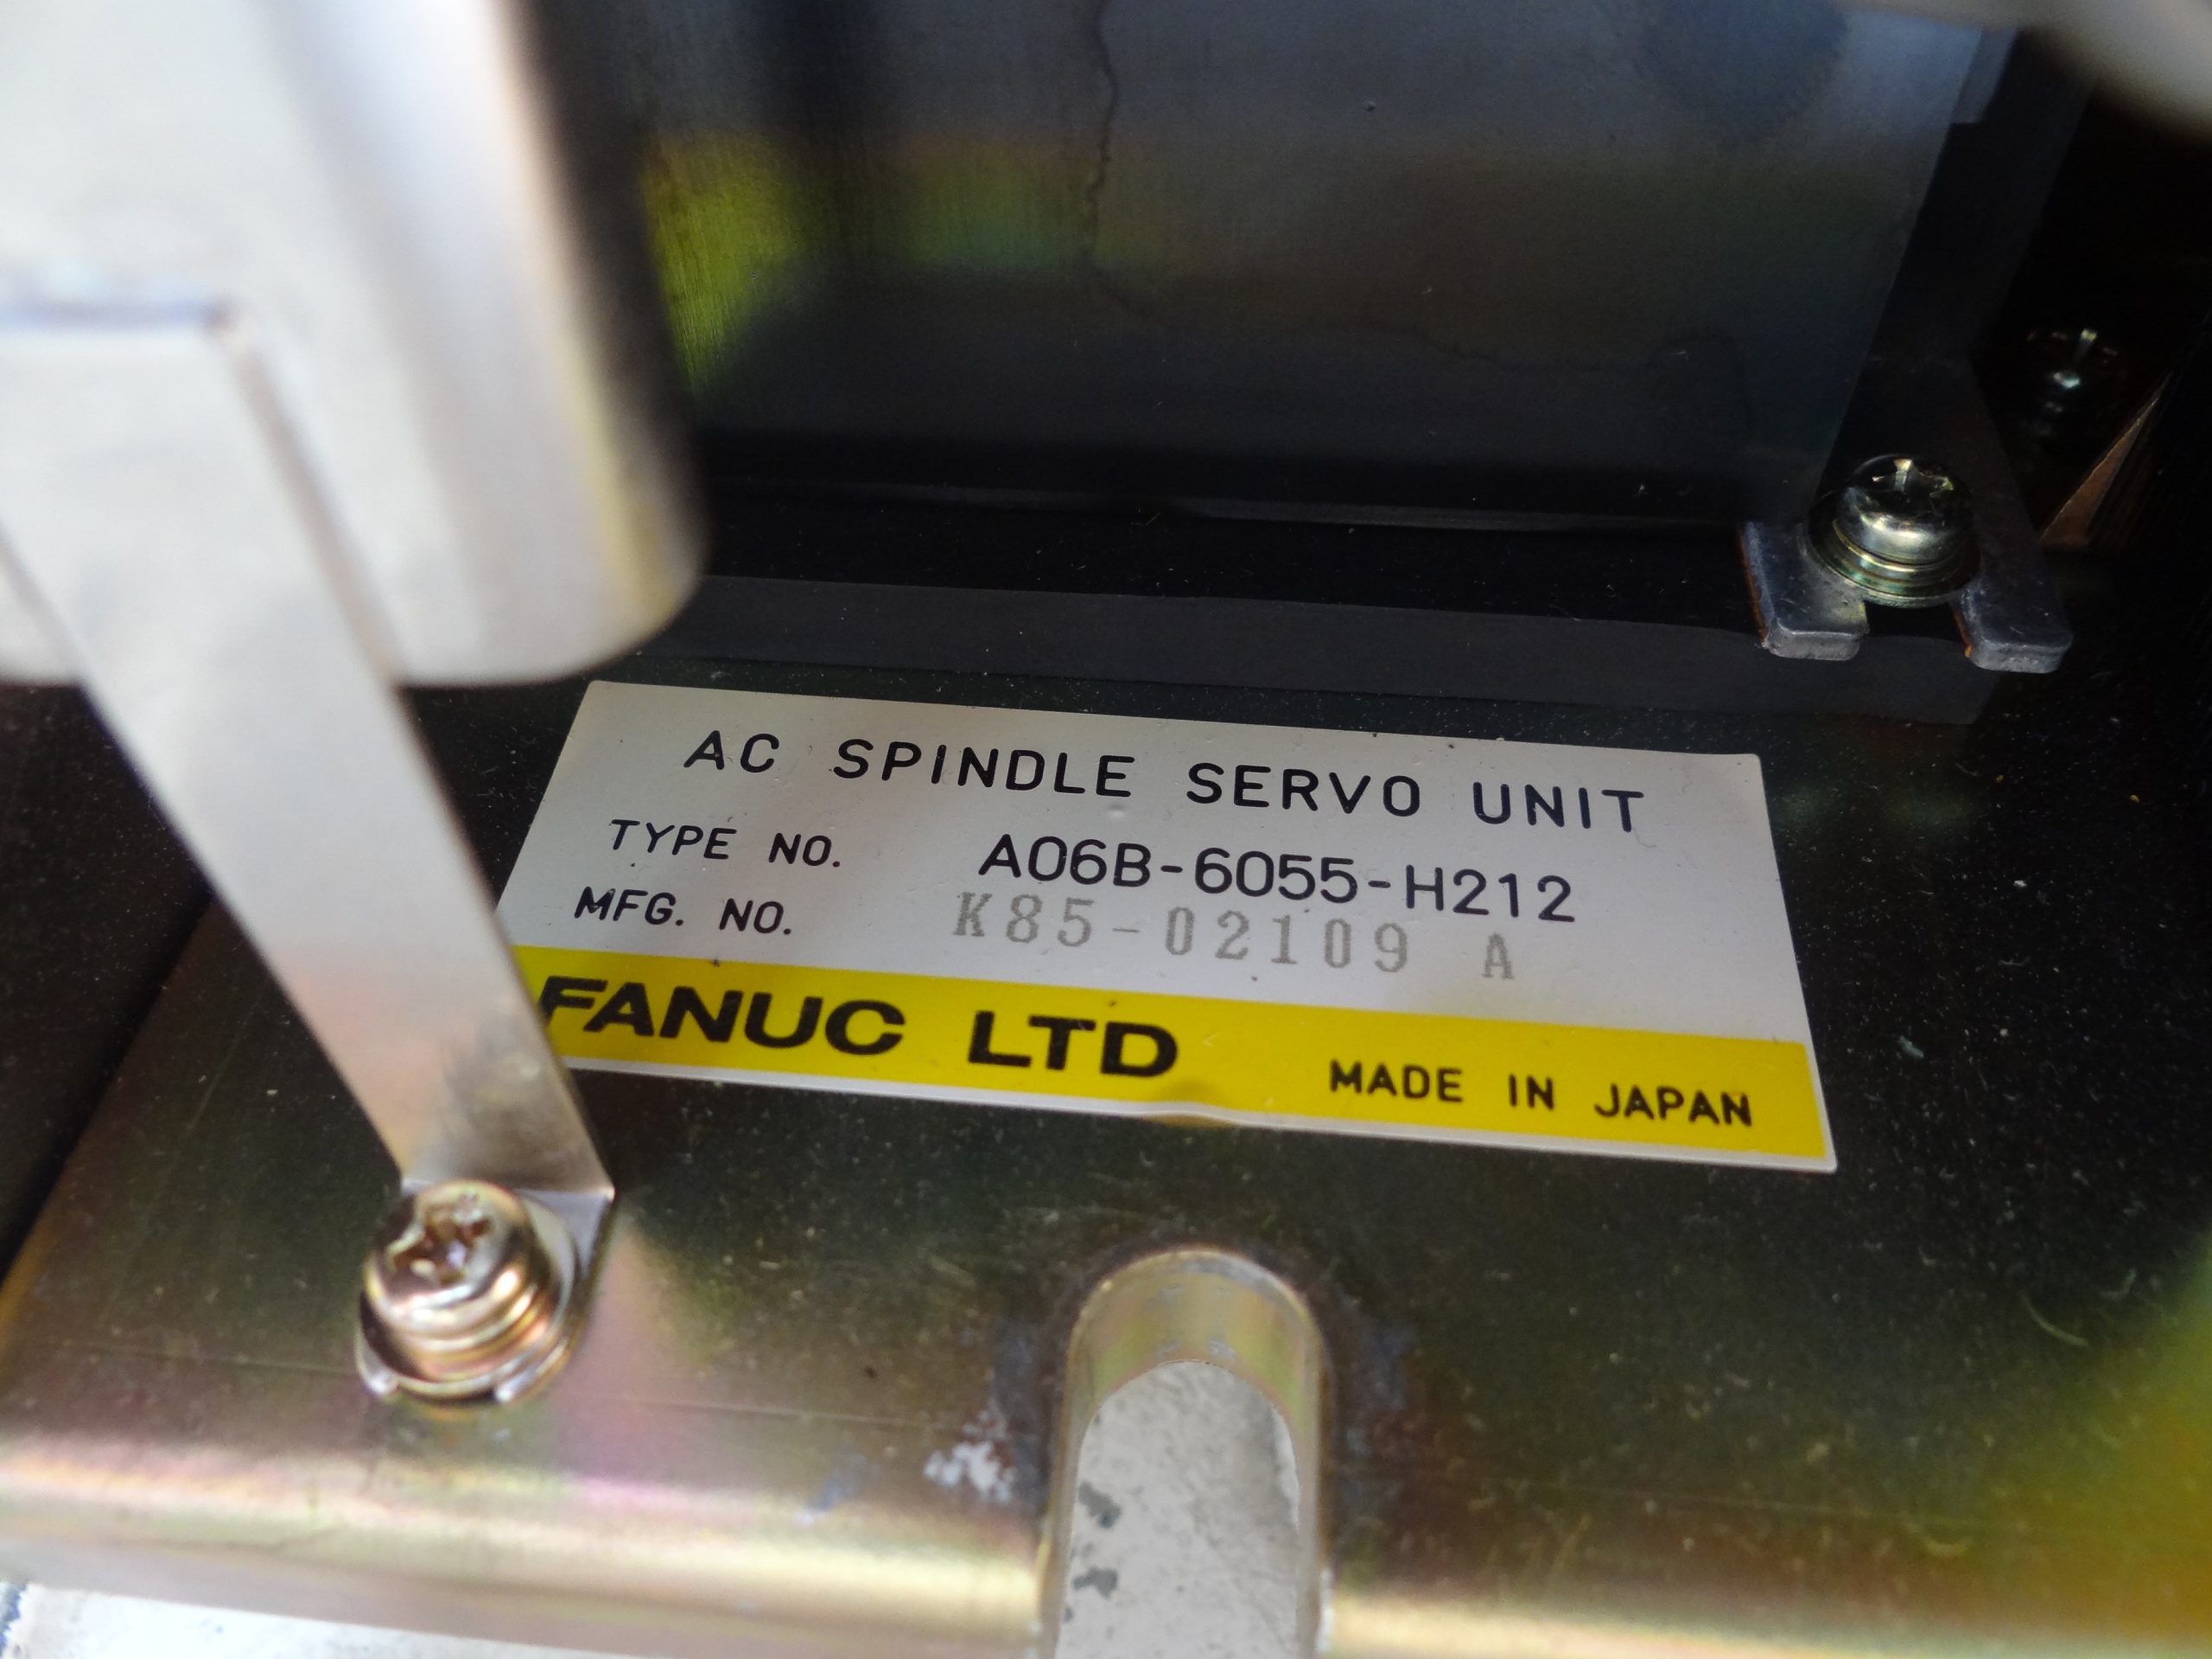 FANUC A06B-6055-H212 nameplate.
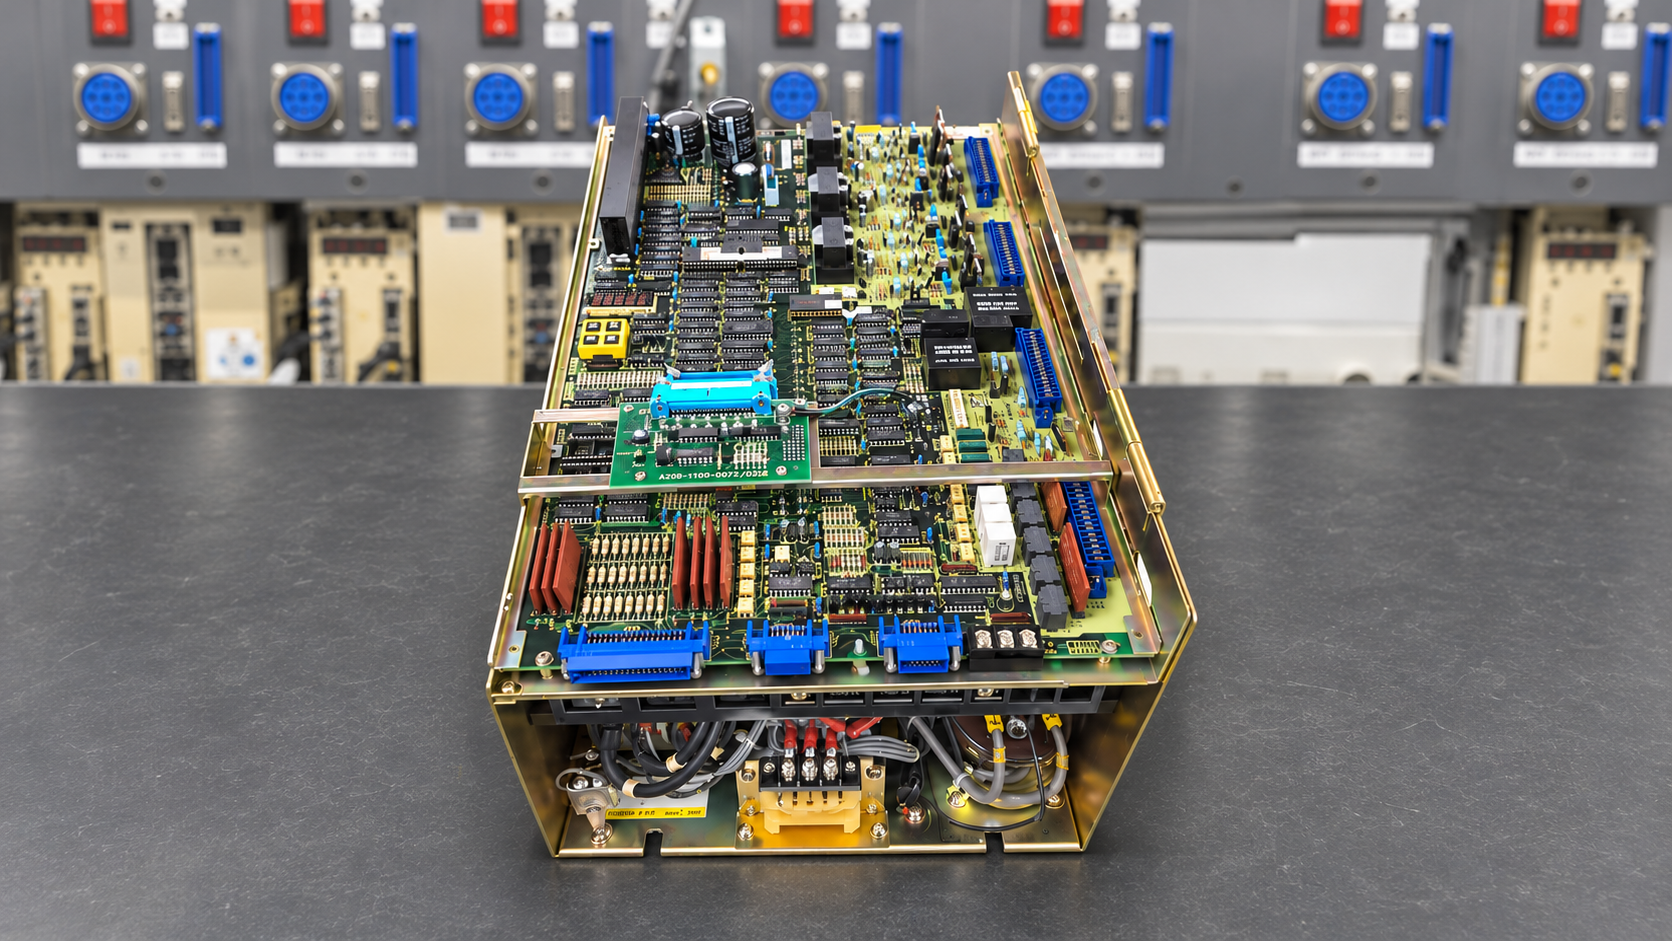 FANUC A06B-6055-H212 after repair.
Request a repair
Need support with a FANUC A06B-6055-H212? Send the complete model designation, exact alarm text and a brief description of when the fault occurs. Industrypart supports the inspection and repair of industrial spindle drives.
FANUC service: https://www.industrypart.com/manufacturers/fanuc
Technical supplement: alarm overview
These general references are diagnostic pointers, not findings from this individual repair. The suggested checks summarise possible areas for investigation.
| Alarm | Meaning in the series documentation | Diagnostic starting point |
|---|
| AL01 | Motor overheating | Check load, motor cooling and temperature monitoring. |
| AL02 | Excessive speed deviation | Investigate load, acceleration and speed feedback. |
| AL03 | DC-link fuse F7 blown | Inspect the power stage and associated control circuitry; include motor and cables. |
| AL04 | AC input fuse blown | Investigate the supply and input section. |
| AL06 | Overspeed, analogue detection | Check speed demand and feedback. |
| AL07 | Overspeed, digital detection | Compare actual speed, settings and control behaviour. |
| AL08 | Supply voltage too high | Check supply voltage and transformer configuration. |
| AL09 | Heat sink overheating | Check airflow, ventilation and thermal load. |
| AL10 | Internal +15 V supply too low | Have the internal supply checked by qualified personnel. |
| AL11 | DC-link voltage too high | Record supply conditions and the operating state. |
| AL12 | Excessive DC-link current | Investigate power stage, motor, cables and load. |
| AL13 | CPU data memory fault | Have the control electronics checked. |
Interpreting symptoms
| Symptom | Possible area to investigate |
|---|
| F7 blows again immediately | Power stage, associated control, motor and cables; do not merely replace the fuse. |
| Fault during acceleration | Load, motor condition, feedback and settings. |
| Fault after warming up | Cooling, environment and temperature-dependent faults. |
| Workshop test satisfactory, fault on the machine | Supply, wiring, mechanical load and feedback arrangement at the installation. |